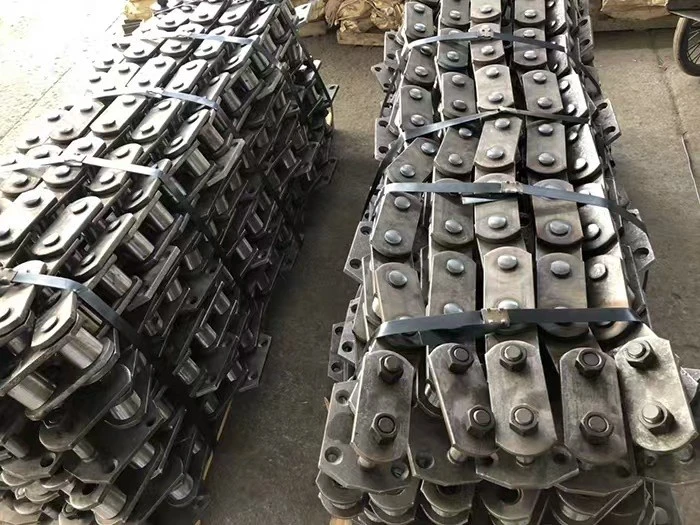
In 2026, the market demand for bucket elevator spare parts keeps stable growth across Southeast Asia. Infrastructure upgrade, grain processing expansion and cement plant renovation drive more inquiries for heavy-duty hoisting chains, including TB NEW hoisting chain.
Local equipment manufacturers tend to replace old lifting chains with upgraded models. They pay more attention to tensile strength, wear resistance and delivery cycle. Safety standard compliance has become a basic requirement for procurement. Buyers no longer only compare unit price; they evaluate total service life and maintenance cost.
As the supply chain shifts, more Southeast Asian importers source heavy-duty chains directly from Chinese chain factories.
TB NEW hoisting chain gains growing attention for stable performance and flexible customization. It can match multiple TB model bucket elevators, saving extra work for equipment modification.
Industry insiders mentioned that manufacturers are optimizing heat treatment technology and surface coating to improve anti-corrosion performance, adapting to high humidity and dusty working conditions in tropical countries. In the future, chains with wear monitoring function will gradually enter the bulk conveying market, helping plant operators reduce unexpected downtime.